Why Choose a Belt Bucket Elevator?
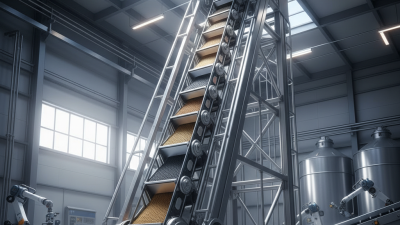
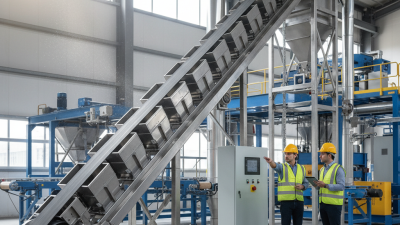
Why choose a Belt Bucket Elevator when materials must travel vertically through limited plant space? This question deserves more than a simple capacity claim. A well-selected Belt Bucket Elevator can move grain, fertilizer, minerals, cement, and other bulk materials with controlled discharge and modest floor requirements. Its continuous belt supports buckets smoothly, reducing sudden impact during conveying.
In practical installations, operators value steady throughput, enclosed material flow, and adaptable lift heights. A food-processing facility may need clean surfaces and easy inspection access. A cement plant may prioritize abrasion resistance, sealed bearings, and dust control. These needs are not interchangeable. Belt speed, bucket spacing, belt strength, inlet design, and discharge geometry must match the material’s moisture, temperature, particle size, and flow behavior. Small design errors can create carryback, slippage, or premature wear.
That is where engineering experience matters. Reliable suppliers review site conditions, duty cycles, maintenance access, and safety requirements before recommending a configuration. They also consider inspection points, belt alignment, guarding, and practical replacement procedures. No elevator is perfect. A belt system may require careful tension monitoring, especially under changing loads. However, proper sizing and routine inspection can support efficient, quiet, and dependable vertical conveying. The best choice is not always the largest machine. It is the system that fits the material, building, operators, and long-term maintenance plan.
Belt Bucket Elevators: Vertical Bulk Conveying at 1–4 m/s
Why Choose a Belt Bucket Elevator?
Belt Bucket Elevators: Vertical Bulk Conveying at 1–4 m/s
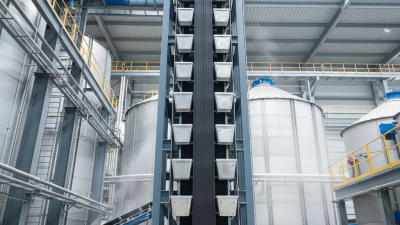
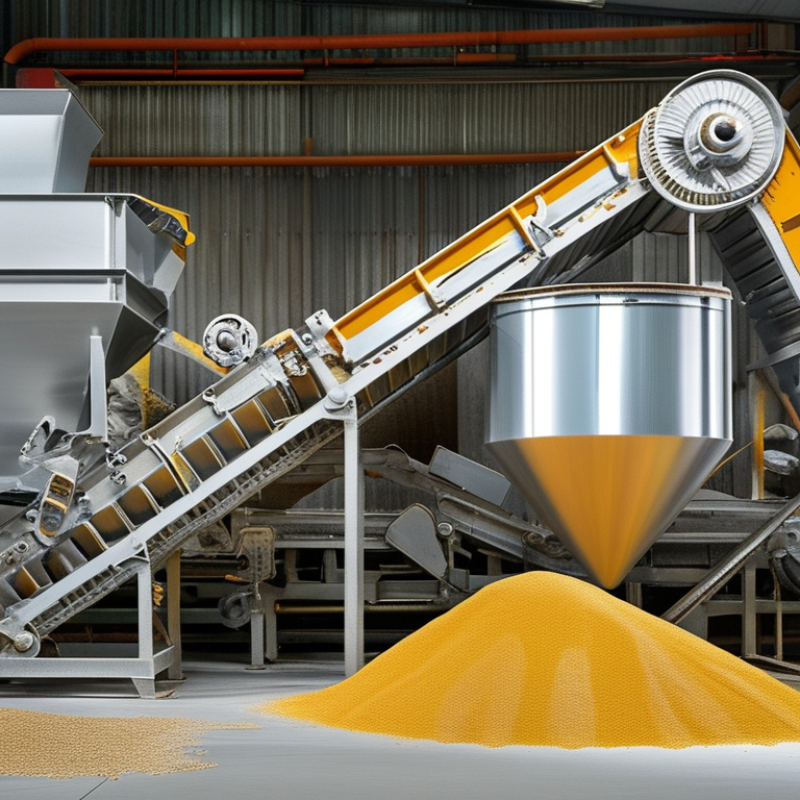
A belt bucket elevator moves bulk material vertically while using limited floor space. Its belt carries attached buckets through a controlled, continuous path. Operating speeds from 1 to 4 m/s cover many practical conveying duties. Lower speeds can protect fragile particles and reduce impact at discharge. Higher speeds may improve capacity when the material flows freely.
Material behavior matters more than speed alone. Grain, fertilizer, pellets, minerals, and powders respond differently inside each bucket. Moisture can cause buildup around the boot section. Dust may require sealed covers, suitable filtration, and regular inspection. Bucket spacing, fill level, belt tension, and pulley diameter must match the intended duty. Small design errors can create slipping, spillage, or uneven loading.
It is not always the fastest option.
Operators should check capacity under real conditions, not only catalog figures. A slightly lower speed may deliver steadier flow and fewer maintenance interruptions. The elevator should also include accessible inspection points, belt alignment monitoring, and protection against overload. These features support safer operation and more reliable performance. Still, no design is maintenance-free. Worn buckets, loose fasteners, and material buildup need prompt attention before they become larger failures.
Capacity and Elevation: Moving Up to 2,000 m³/h Over 60 m
Why Choose a Belt Bucket Elevator?
Capacity and elevation define whether a belt bucket elevator earns its place in a bulk-handling line. A belt bucket elevator can move up to 2,000 m³/h and lift material more than 60 m, when properly engineered. That figure is not automatic. Bulk density, particle size, moisture, bucket spacing, and loading conditions all affect real throughput. CEMA’s Belt Conveyors for Bulk Materials, 7th Edition, emphasizes these variables when calculating conveying capacity.
The vertical route saves valuable floor space. It also reduces transfer points, dust release, and product degradation in many applications. A steady stream of mineral, grain, or fertilizer can rise inside a compact casing, rather than travel through several horizontal conveyors. The details matter. A poorly filled bucket may waste installed capacity. Excessive belt speed can increase wear and material impact.
Energy deserves attention too. The U.S. Department of Energy reports that motor-driven systems consume about 70% of industrial electricity. Efficient drives, correct tension, and suitable bucket loading can reduce avoidable losses. However, I would not select an elevator from capacity alone. A 2,000 m³/h specification may look impressive, yet the actual duty could be much lower. Material tests and site measurements should confirm the design. Even experienced engineers can underestimate moisture changes. That mistake becomes expensive at 60 m.
Energy Efficiency: Continuous Transport With Lower Chain Friction
Why Choose a Belt Bucket Elevator?
A belt bucket elevator moves bulk material vertically in a steady, controlled flow. Unlike many chain-driven systems, it uses a flexible belt instead of repeated metal links. This reduces chain contact, sprocket engagement, and friction-related energy loss. The difference becomes noticeable during long operating hours. A motor lifting grain, powder, or small aggregates can run more smoothly when resistance stays lower. Noise may also decrease. That matters in enclosed production areas.
From practical maintenance experience, energy savings depend on more than the belt itself. Correct tension, balanced loading, and clean pulleys are essential. A misaligned belt can rub against the casing and waste power quickly. Overfilling buckets creates another problem. It increases starting load and may cause material to spill. A properly selected elevator can provide continuous transport with fewer sudden movements. Still, it is not an automatic solution. Poor installation can erase much of its efficiency advantage.
Tips: Check belt tension regularly, inspect pulley alignment, and remove buildup from buckets and casing. Record motor current during normal operation. A gradual increase may reveal friction, overloading, or worn components before failure occurs. Keep the inspection notes simple and consistent. Small details are easy to miss.
Why Choose a Belt Bucket Elevator?
Energy Efficiency: Continuous Transport With Lower Chain Friction
The chart compares representative specific energy demand for belt and chain bucket elevators operating at the same lifting height and material throughput. Belt systems generally require less energy because flexible belts reduce friction, impact, and moving-part resistance during continuous transport.
Representative engineering benchmark in kWh per metric ton; actual values vary with lift height, material properties, elevator speed, loading efficiency, and maintenance condition.
Material Handling: Supporting Particles up to 50 mm and 90°C
Why Choose a Belt Bucket Elevator?
Material handling becomes demanding when particles reach 50 mm and temperatures approach 90°C. A belt bucket elevator can move this load vertically with controlled discharge and limited floor space. Its enclosed path also reduces dust escape around transfer points. Less spillage means cleaner platforms and fewer manual interventions.
The application still needs careful engineering. Bucket spacing, belt tension, feed rate, and particle shape affect capacity. CEMA guidance links elevator performance to bulk density, belt speed, and loading conditions. These details matter more than a simple size claim. A 50 mm limestone piece may behave differently from a damp fertilizer granule. Testing is wise.
Energy also deserves attention. The International Energy Agency’s Energy Efficiency 2023 report states that industry used about 37% of global final energy in 2022. Efficient vertical conveying can therefore support lower operating demand, although actual savings depend on lift height and duty cycle. The U.S. Geological Survey reported approximately 4.1 billion metric tons of global cement production in 2022. That scale shows why reliable hot-material handling matters. At 90°C, belt compounds, bucket fasteners, bearings, and cooling time require verification. We should not assume one configuration fits every plant.